EN
 FR
 DE

Tiana
+86-13143789995
4.8 Alibaba Rating, Get a Quote in 2 Hours Activate now
Request a Free Physical Sample Find Us
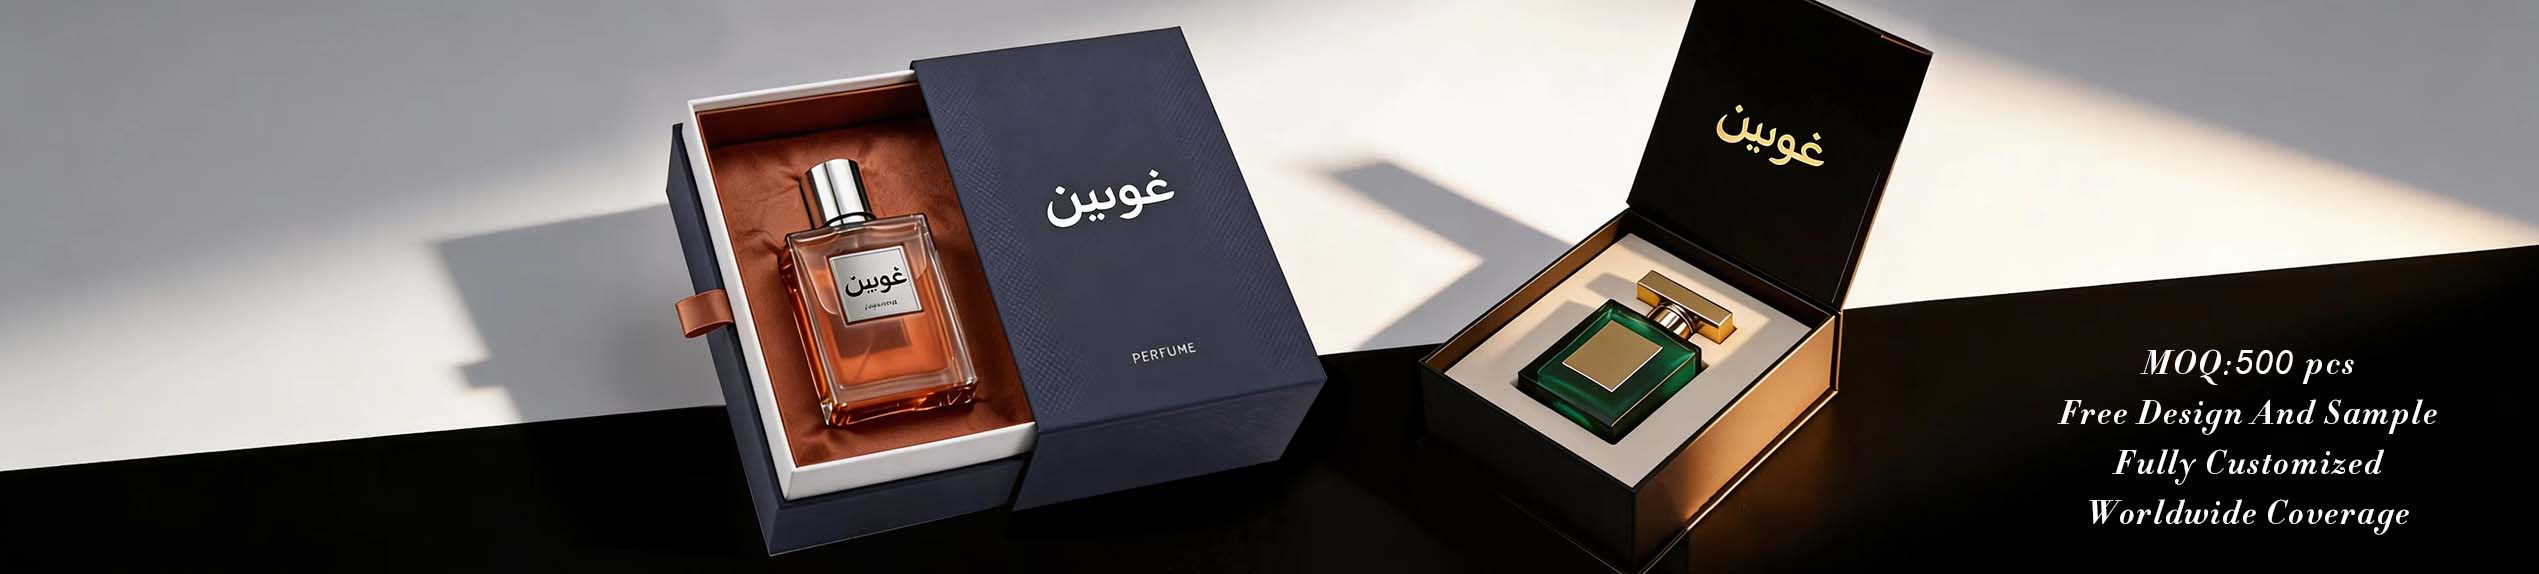
How to Solve Real Packaging Problems for Premium Brands
For premium brands, a scratch, a misaligned foil, or a transit-damaged box is a review and a return. This engineering view fixes three real failure modes — surface scratching, foil/closure misalignment, and transit damage — with the concrete controls that keep them out of your run.
Premium brands live or die by the unboxing. A scratch on a matte lid, a misaligned foil logo, or a caved-in box after transit is not a 'minor defect' — it is a review, a return, and a dent in brand equity. This article works three real failure modes from a factory-engineering view: surface scratching, foil/closure misalignment, and transit damage, with the concrete fixes that keep them out of your run.
What this guide covers
our certifications lists what has been independently verified.
Soft-touch and matte laminations look luxurious precisely because they show every mark. Scratches usually enter at three points: the wrapping station, interleaving, and the pack-out carton. The fix is process, not material luck.
From the factory floor
On a recent soft-touch run we cut rub-mark rejects from 4.1% to 0.6% by adding glove-only handling plus glassine interleaving — a process change, not a material upgrade.
Spec the liner: 120 gsm kraft, non-abrasive side facing the product.
A foil logo 0.4 mm off its emboss, or a magnetic lid that closes 1.5 mm proud, reads as 'cheap' on a premium shelf. Misalignment is a registration and tooling problem, solved with tighter tolerances and camera inspection.
Foil registration drifts when the web tension varies or the die heats unevenly. Hold it with a calibrated hot-foil press (110–140°C, controlled dwell) and in-line camera reject past ±0.2 mm. A manual eyeball at the end of the line misses the slow drift that ruins box 8,000 of 10,000.
Magnetic lids sit proud when the magnet pocket is cut 0.3 mm off or the wrap stretches during mounting. Fix by cutting magnet pockets to ±0.5 mm on a CNC, verifying wrap tension, and sampling pull force (≥ 3 N) on a tensometer per batch. A lid that closes true is a function of pocket accuracy, not glue.
warn
If your supplier answers 'foil alignment is hand-checked' — walk away for a premium run. Human end-of-line checks cannot catch the gradual web drift that misaligns foil across a long run. In-line camera reject at ±0.2 mm is the only reliable control.
Table 1. The four premium-defect tolerances and the control that holds each — write them into the PO.
| Defect | Tolerance to hold | Control |
|---|---|---|
| Foil vs emboss offset | ±0.2 mm | Calibrated hot-foil + in-line camera reject |
| Lid closure proud | ≤ 0.5 mm | CNC magnet pocket ±0.5 mm, wrap tension check |
| Magnet pull force | ≥ 3 N | Tensometer sampling per batch (AQL) |
| Surface rub mark | ≤ AQL 1.5 | Glove handling + glassine interleave |
A perfect box that arrives caved-in is still a failure. Transit damage comes from inadequate board grade, weak corners, and poor palletisation — all fixable before the container seals.
Specification
Validate the carton to ISTA 3A (distribution simulation) and a 1.2 m drop before launch.
Compression: limit pallet stack height to the load the 1.5–2.0 mm board is validated to carry.
We go deeper on this in Luxury Packaging Manufacturing.
The three problems above share one cause: quality left to chance instead of built into the line. A prevention system ties them together with documented controls and sampling.
tip
For a launch-critical SKU, pilot 500–1,000 units and 100% inspect 50 of them against Table 1 before the full run. The pilot converts every 'should be fine' into a measured fact — and protects the unboxing that your marketing budget paid for.
FAQ
Why do scratches appear only after shipping, not at the factory?
Because they are caused by inter-box rub and abrasive carton liners during transit — not at the clean finishing line. Interleaving and a non-abrasive liner are the fixes, and they only show up once the box is jostled for two weeks.
How tight must foil registration be for premium?
±0.2 mm against the emboss or print below it. Beyond that the eye reads 'off', especially on a large logo. Hold it with in-line camera reject, not end-of-line hand checks.
My magnetic lid closes proud — what is wrong?
Almost always a magnet pocket cut off by 0.3 mm or wrap stretch during mounting. CNC the pocket to ±0.5 mm and verify wrap tension; the lid then seats true without extra glue.
How do I prove transit durability before launch?
Require ISTA 3A distribution simulation plus a 1.2 m drop test on a sample carton, and limit pallet stack height to the validated compression load. A supplier who cannot produce these tests is guessing.
What AQL should a premium run use?
AQL 1.5 for cosmetic defects (scratch, foil, rub) on prestige work; AQL 2.5 is the floor for general. Insist the plan cites ISO 2859-1 so it is a real sampling scheme.
Ship premium boxes that arrive perfect
GooinPack builds the prevention system into the line: glove handling, glassine interleaving, in-line foil camera reject at ±0.2 mm, tensometer closure sampling, and ISTA 3A validation. Tell us your failure mode and we will show the control.
Request a QuoteReferences


Blog Sitemap Xml Privacy Policy
Copyright © 2026 GuangZhou GooinPack Packaging Co., Ltd. All Rights Reserved.  Network Supported
Friendly Links: Blogger
Leave A Message
Scan to WhatsApp :